

PVC Celuka Foam Board
Celuka board holds screws at 900N or more, with a Shore D65 hard skin, clean CNC edges that need almost no sanding, and PUR edge banding that bonds to the skin like it belongs there.
Density from 0.50 to 0.80 g/cm³, thickness from 1 to 40 mm, bending strength ≥18 MPa, DIN 4102 B1. It suits bathroom vanities, kitchen cabinets, office furniture, interior cladding, and CNC-routed signage.
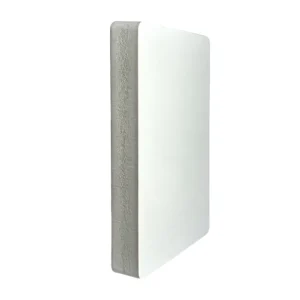
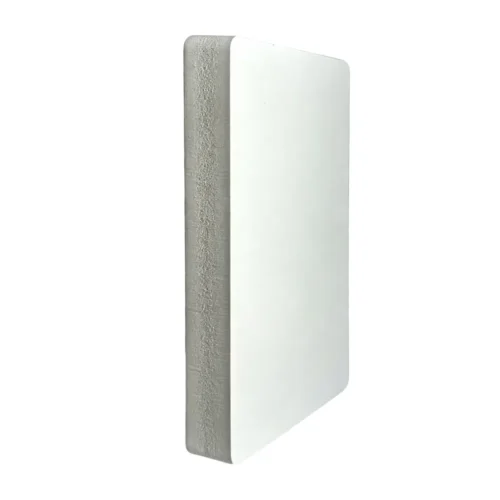
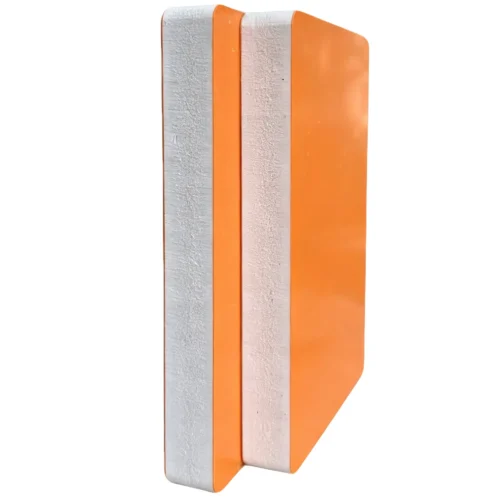
The skin and core come from the same extruder, so the cut edge is one uniform surface, not a white skin wrapped around a grey core.
0.35–0.80
Density
1–40 mm
Thickness
D65
Shore
≥900N
Screw Holding
Why cabinet and furniture makers switch to Celuka foam board
MDF swells in bathrooms Every time.
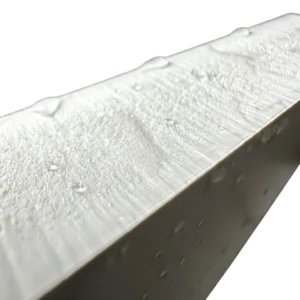
A bathroom vanity made from moisture-resistant MDF still fails. Not immediately. Twelve to eighteen months in, the edges begin to swell. The veneer peels. The doors stop closing. The customer calls. The replacement costs more than the original job was worth. Celuka foam board has a closed-cell structure. The closed-cell structure helps keep water out, so dimensions stay more stable in humid conditions than MDF.
Formaldehyde compliance is no longer optional
MDF and particleboard rely on urea-formaldehyde resin. The EU has been tightening formaldehyde limits for years. Some buyers only discover their cabinets fail the standard when the shipment reaches customs. PVC foam board contains no formaldehyde-based binder. Emissions fall below the EN 717-1 detection limit and comply with GB/T 39600 E0 grade. If the destination market is Europe or North America, the compliance argument alone covers the material cost difference.
Manufacturing Process
Definition and Basic Structure
The Celuka process centres on a metal torpedo inside the die. It occupies space within the melt flow, leaving a hollow cavity as the material exits. A chilled sizing plate sits directly against the die exit. The melt surface drops from approximately 190 degrees Celsius to below 70 degrees within 0.5 to 1 second. The surface PVC chains freeze instantly into a dense arrangement. The blowing agent has no time to decompose. This frozen surface is the hard skin. It is smooth, dense, and measures Shore D65.
The core stays at 180 to 190 degrees. The blowing agent decomposes and releases gas. With the surface already frozen solid, the gas can only expand inward, filling the cavity left by the torpedo. This inward foaming generates counter-pressure that helps produce a uniform closed-cell structure.
Skin thickness is controlled by torpedo size and cooling intensity, typically ranging from 0.1 to 1 millimetre. Overcooling creates residual stress that leads to warping. Undercooling produces insufficient surface hardness. Die temperature, extrusion speed, and cooling water temperature must be precisely matched.
The B1 fire rating comes from an antimony trioxide and zinc borate synergistic system. Antimony trioxide captures combustion radicals in the gas phase. Zinc borate forms a glassy protective layer on the surface and releases crystal water at approximately 290 degrees Celsius to absorb heat, while also suppressing the smoke density caused by antimony trioxide. Together they raise the limiting oxygen index from 23 percent to between 28 and 34 percent. Total flame retardant loading ranges from 15 to 45 parts per hundred parts of PVC resin.
ACR processing aid, with a molecular weight of 500,000 to 1.2 million, forms a three-dimensional entanglement network with the PVC chains to build melt strength. When melt strength is insufficient, foaming gas pressure ruptures cell walls, causing coalescence. The cross-section reveals large cells or visible cavities.
Manufacturing sequence: raw materials are mixed in a high-speed mixer to approximately 120 degrees Celsius for uniform dispersion, then transferred to a low-speed cooling mixer and brought down to 40 to 50 degrees. A conical twin-screw extruder plasticates the compound, rising from approximately 160 degrees in the feed zone to 190 degrees at the metering zone. The melt passes over the torpedo to create the hollow core, the surface freezes against the sizing plate to form the skin, and the core foams inward to fill the cavity. A vacuum calibration table sets the final thickness and flatness. A caterpillar haul-off pulls the sheet at a steady speed, and an automatic saw cuts it to the standard 1220 by 2440 millimetre panel size. Optional double-sided sanding holds thickness tolerance within plus or minus 0.2 millimetres. PE protective film can be applied before warehousing.
How to Identify Celuka Board
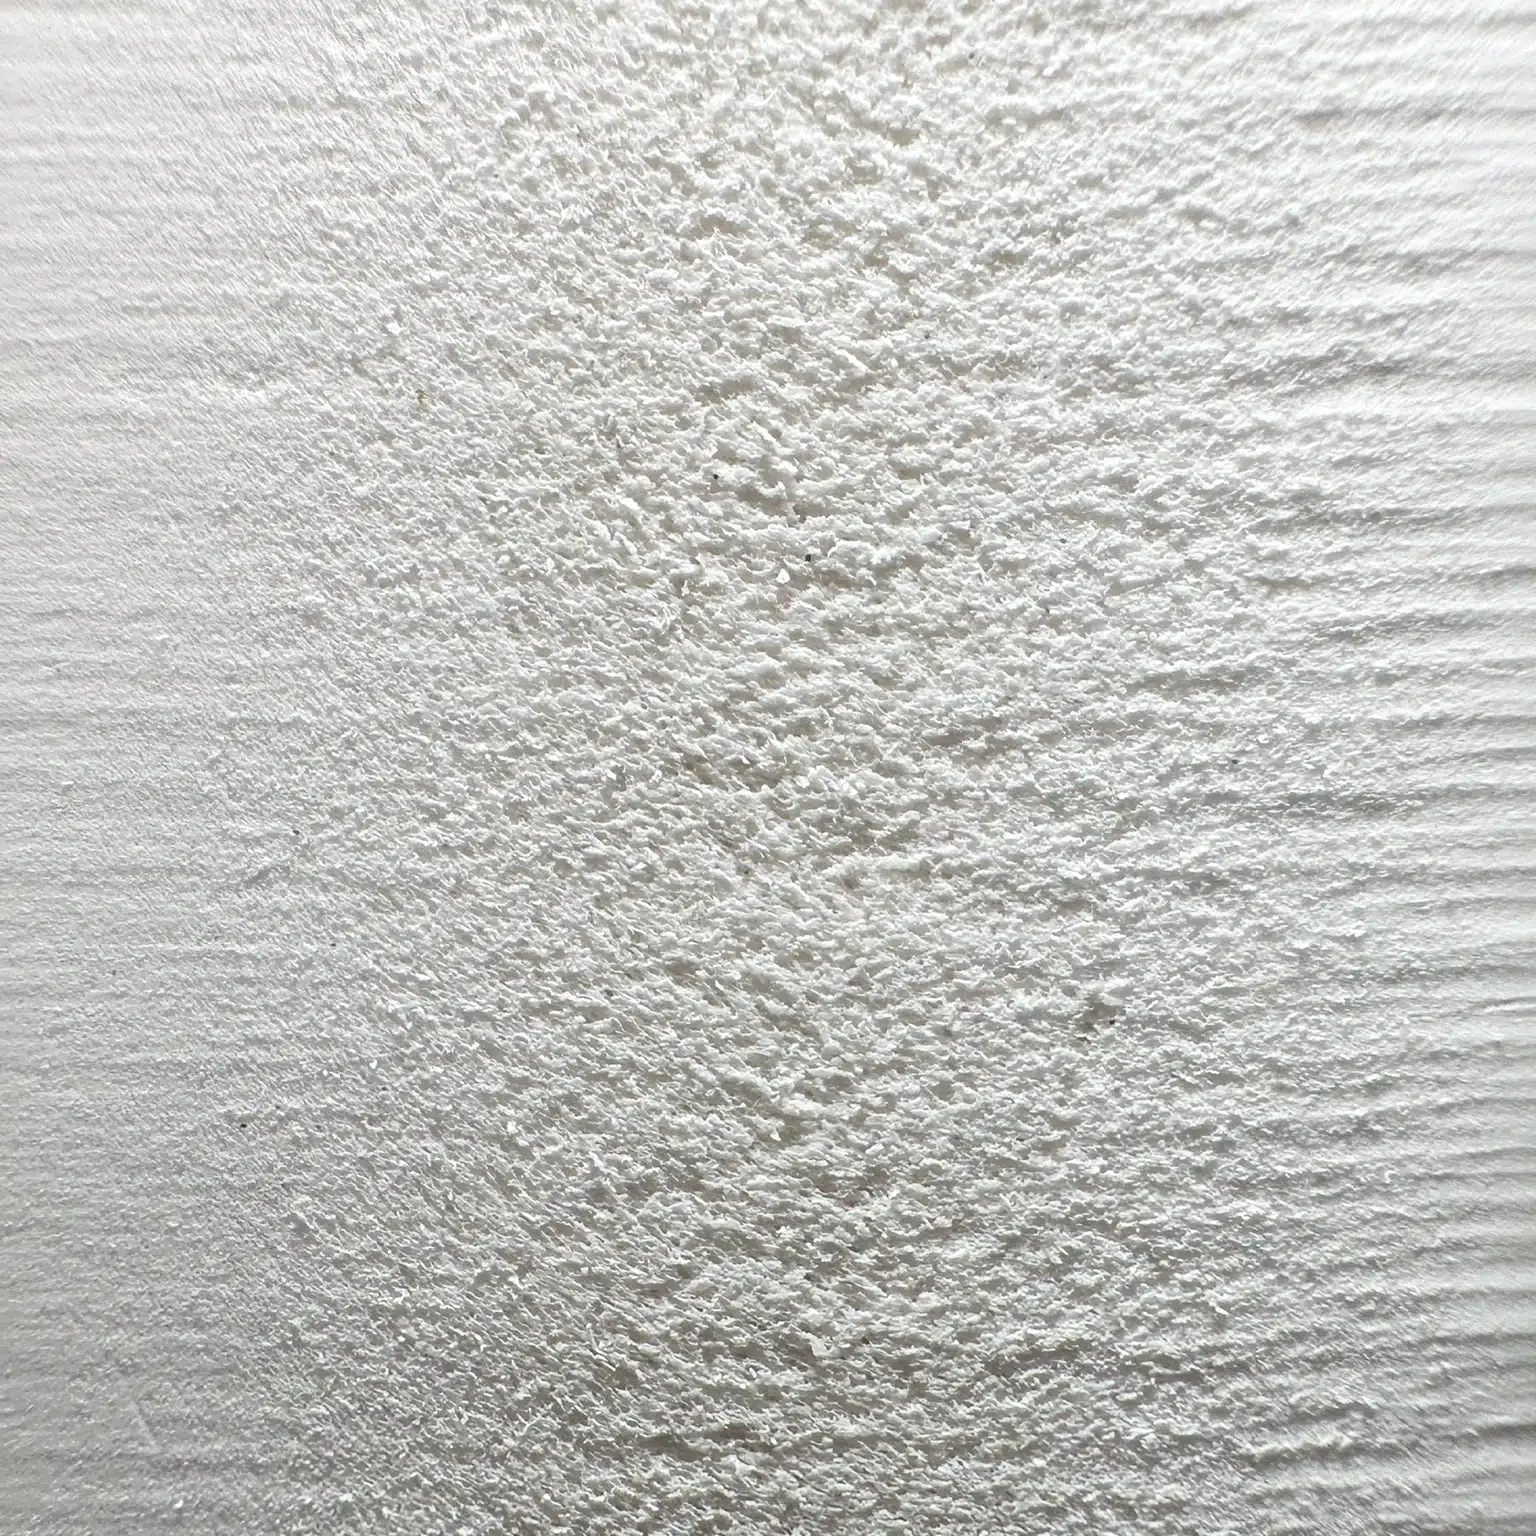
Place the board under natural light.
The surface is smooth and glossy. It reflects light. This is the most immediate sign of the hard skin. A fingernail drawn across the surface detects no texture. The skin is dense, with a hardness of Shore D65.
Cut a small piece and examine the cross-section.
This is the most reliable identification method. The layered structure is clear: a dense hard skin on both faces, 0.1 to 1 millimetre thick, slightly darker in colour than the core. The core is a foam structure with fine, uniform closed cells. There is no glue line between the skin and the core. Both are the same PVC resin, the same formulation. The difference in structure comes only from the difference in cooling speed. Under magnification, the transition from skin to core is continuous. There is no abrupt interface.
Run it through a CNC router or saw.
Inspect the cut edge. Because the hard skin is present, the cut line comes out clean with no fuzz. This is a direct benefit of the skin, and it is the most practical quick check on the shop floor.
Technical Specifications
| Parameter | Data | Industry Reference |
|---|---|---|
| Thickness | 1 mm to 40 mm | 1 mm to 40 mm |
| Density Range | 0.35 to 0.80 g/cm³ | Low density = lighter and cheaper. High density = stiffer |
| Standard sizes | 1220×2440mm, 915×1830mm, 1560×3050mm, 2050×3050mm | 1220×2440mm, 915×1830mm, 1560×3050mm, 2050×3050mm |
| Flexural Strength | White, black, red, blue, yellow, green, grey; custom color matching available | — |
| Flexural strength | ≥ 18 MPa | 12 to 25 MPa, density-dependent |
| Shore Hardness | D65 | D60 and above |
| Maximum Continuous Service Temperature | Factory data ≥ 70°C | HDT@264 psi approx. 63°C |
| Service temperature | Up to 65°C | Do not place near heat sources or use dark-coloured sheets in direct sunlight |
| Vicat Softening Point | 73 to 82°C, typical approx. 75°C | — |
| Colors | White, black, red, blue, yellow, green, grey; custom color matching available | — |
Specification Notice: The technical data above represent typical values from Shine’s internal testing and industry references. Test standards are cited where applicable. Actual values depend on board density, thickness, color, and production batch. For critical applications, request batch-specific test data from our technical team. Third-party testing is available at the buyer’s request and expense.
Processing Guide
The hard skin of Celuka is 0.1 to 1 mm thick, at Shore D65 hardness. When a milling cutter passes through, it shears cleanly; sanding is required before bonding, and hot‑bending temperatures are higher than for free‑foam boards. Used correctly, the hard skin is an advantage; used wrongly, it is an obstacle.
CNC Machining and Saw Cutting
Edgebanding: The edgeband width should be board thickness plus 2 to 4 mm. Hot air at 180 to 200°C, feed speed 15 to 20 m/min. After trimming, chamfer to R0.5 to 1.0 mm. Quality depends on the flatness of the sawn edge and the activation temperature of the adhesive.
PUR lamination: Before lamination, sand the hard skin with 400‑grit sandpaper, blow off dust with compressed air, and wipe with isopropanol to remove grease. Apply PUR adhesive at 120 to 140°C in molten form, with pressure 0.3 to 0.5 MPa and pressing time 10 to 30 seconds. Under room temperature above 15°C and relative humidity above 40%, final bond strength is reached in 3 to 7 days. Insufficient humidity leads to incomplete curing.
Edge Banding, Lamination and Surface Bonding
Painting: Before painting, sand the hard skin with 200 to 400 grit sandpaper. If you skip sanding, the paint will peel. Use only water‑based acrylic or latex paints; oil‑based and solvent‑based paints will attack PVC. Apply a plastic‑specific primer first, then apply multiple thin topcoats. Allow each coat to dry before the next; full curing takes 30 days. Do not paint when humidity exceeds 80%. For dark boards being painted light, first apply a white blocking primer.
UV printing: Before printing, ensure the surface energy is not less than 38 dynes/cm. Celuka as supplied is only 34 to 36. Treat with corona to 40 to 44 and print immediately after treatment. Skip this step, and the ink will peel after a few months.
Surface finishing: The hard skin of Celuka can be used directly as the finished surface. The cross‑section has uniform colour from skin to core with a smooth density gradient, requiring no lamination or edgebanding.
For Celuka‑to‑metal, use epoxy resin; roughen the metal surface by coarse sanding and apply a primer. For Celuka‑to‑acrylic, use methyl methacrylate structural adhesive. Do not use woodworking PVA glue.
Painting, Coating and Surface Finishing
Painting: Before painting, sand the hard skin with 200 to 400 grit sandpaper. If you skip sanding, the paint will peel. Use only water‑based acrylic or latex paints; oil‑based and solvent‑based paints will attack PVC. Apply a plastic‑specific primer first, then apply multiple thin topcoats. Allow each coat to dry before the next; full curing takes 30 days. Do not paint when humidity exceeds 80%. For dark boards being painted light, first apply a white blocking primer.
UV printing: Before printing, ensure the surface energy is not less than 38 dynes/cm. Celuka as supplied is only 34 to 36. Treat with corona to 40 to 44 and print immediately after treatment. Skip this step, and the ink will peel after a few months.
Surface finishing: The hard skin of Celuka can be used directly as the finished surface. The cross‑section has uniform colour from skin to core with a smooth density gradient, requiring no lamination or edgebanding.
Thermoforming, Bending and Fastening
Hot bending: Heat uniformly to 70 to 120°C. For precision hot bending, 115 to 125°C is recommended, with segmental heating to ensure the core reaches temperature, not just the surface. Minimum bending radius is 2 to 3 times board thickness. After bending, hold the shape and cool naturally; do not quench with water. For complex curves, prepare moulds in advance to assist shaping.
Fastening: Pilot holes must be pre‑drilled. Driving self‑tapping screws directly will split the core. Use wide‑thread wood screws and do not overtighten. Screw holding specifications: see Product Features > Screw Holding Strength.
When installing, note that PVC’s linear thermal expansion coefficient is about 0.07 mm/m·°C. Stud spacing should not exceed 400 mm. Use stainless steel screws with pre‑drilled holes at 200 to 300 mm spacing.
Laser cutting is absolutely prohibited: PVC contains chlorine, and the high temperature of the laser releases hydrogen chloride gas, which is toxic and corrosive to equipment. There are no exceptions.
Request Celuka Samples for Testing
Processing parameters are a starting point. Your machine, your tooling, and your shop conditions determine the final results. Request samples in your preferred thickness, density, and color.
Applications
Furniture Manufacturing
The bathroom is the highest‑humidity space in a residential building. Traditional boards absorb moisture in wet environments, causing edgebanding to crack and hinges to loosen. The closed‑cell structure of PVC does not absorb water, and screw‑holding power remains unchanged under humid conditions. This is not a comparison of strength under dry conditions, but of stability under wet conditions.
For cabinet bodies, use Celuka 15 to 18 mm, density 0.55 to 0.65 g/cm³ (screw holding specifications: see Product Features). Pre‑drill pilot holes, use wide‑thread wood screws, and do not overtighten. For doors, use 5 to 10 mm, with PUR‑laminated decorative facing and matching PVC edgebanding.
Kitchen cabinets share the same parameters as bathroom cabinets; note that surface finishes must be resistant to cleaning agents. For office furniture, B2 flame‑retardant grade can be used, with density reduced to 0.50 to 0.60 to lower material costs. Load‑bearing requirements in office environments are lower than in cabinets, and the dry environment does not mandate waterproofing.
Outdoor Signage and Display Structures
The role of Celuka in the advertising industry is not as a printing substrate. For printing, free‑foam board is cheaper and more convenient. Celuka is positioned for CNC engraving and for signs that require structural strength.
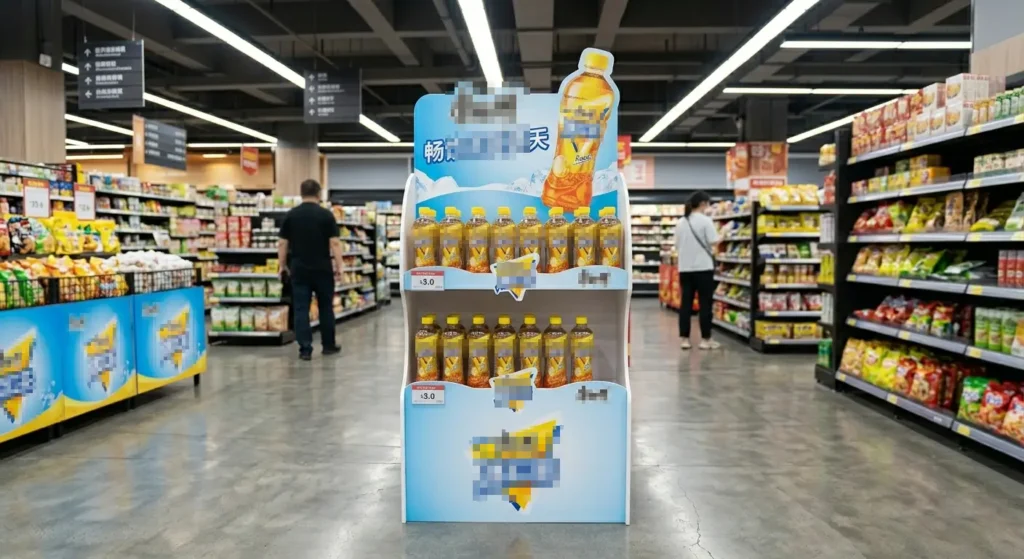
3D engraved letters and logos represent the most typical advertising application for Celuka. The hard skin shears cleanly as the tool passes, and edges require no sanding. Use 5 to 10 mm thickness, density 0.50 to 0.60, with a single‑flute O‑flute router bit for direct engraving. POP display stands also use Celuka 5 mm, CNC‑cut plus UV printing, offering greater durability than free‑foam board.
For outdoor commercial signs, choose Celuka 8 to 10 mm; the thickness allows room for expansion gaps. Dark‑coloured boards absorb heat under direct sunlight – remember to reserve expansion gaps of 3 to 5 mm per metre. If the sign needs to serve outdoors for more than 7 years, choose co‑extruded board rather than Celuka. Fire rating and outdoor service life details: see Product Features and Technical Specifications.
Architectural Decoration
Architectural decoration is the largest global application segment for Celuka.
For interior wall cladding, use Celuka 8 to 12 mm, density 0.50 to 0.60. Fire-rated options available where building codes require (see Product Features for B1 details). Stud spacing should not exceed 400 mm; fix with stainless steel screws in pre‑drilled holes, and reserve expansion gaps of 5 to 8 mm every 3 metres. The thermal expansion coefficient of PVC is 0.07 mm/m·°C – failure to leave gaps will result in panel warping.
For office partitions, use 12 to 15 mm. Single‑layer sound insulation is approximately 25 dB STC; double‑layer with a 50 mm cavity and acoustic insulation can reach 35 to 40 dB STC. The cross‑section of Celuka has uniform colour from skin to core, requiring no edgebanding or veneering, and can be used directly as the finished surface of the partition.
For ceilings, use 8 to 12 mm, density reduced to 0.45 to 0.55. Lightweight and water‑resistant – traditional gypsum board is damaged by water, while Celuka ceilings do not require replacement after pipe leaks.
Concrete formwork is a special application of Celuka. High‑density Celuka 0.60 to 0.80, 15 to 18 mm thick, can be reused 20 to 60 times, depending on the formulation and cleaning/maintenance after demoulding. The per‑use cost is less than half that of wood formwork. After demoulding, rinse with clean water – no release agent is required. This is not permanent formwork, but reusable turnover formwork.
Retail and Store Fixtures
Retail shelving and display tables require boards whose edges can be left exposed without secondary edge treatment. The hard‑skin cut edge of Celuka is the finished surface – uniform in colour, with no demarcation line. Use 8 to 12 mm thickness, density 0.50 to 0.65. The board can be hot‑bent into curved shapes, CNC‑engraved with brand logos, and laminated with metal‑brushed or wood‑grain foils.
For pop‑up store wall panels, use Celuka 5 to 8 mm without secondary surface finishing, enabling quick assembly and disassembly. If extreme light weight and low cost are required, 3 to 5 mm free‑foam board is an alternative. The advantage of Celuka lies in its resistance to scratches after repeated assembly and disassembly, allowing multiple reuse cycles.
Not Sure If Celuka Fits Your Specific Application?
Each industry has its own requirements for density, thickness, fire rating, and processing. Whether you are manufacturing furniture, installing wall cladding, or routing 3D signage, our technical team can provide spec recommendations tailored to your production environment.
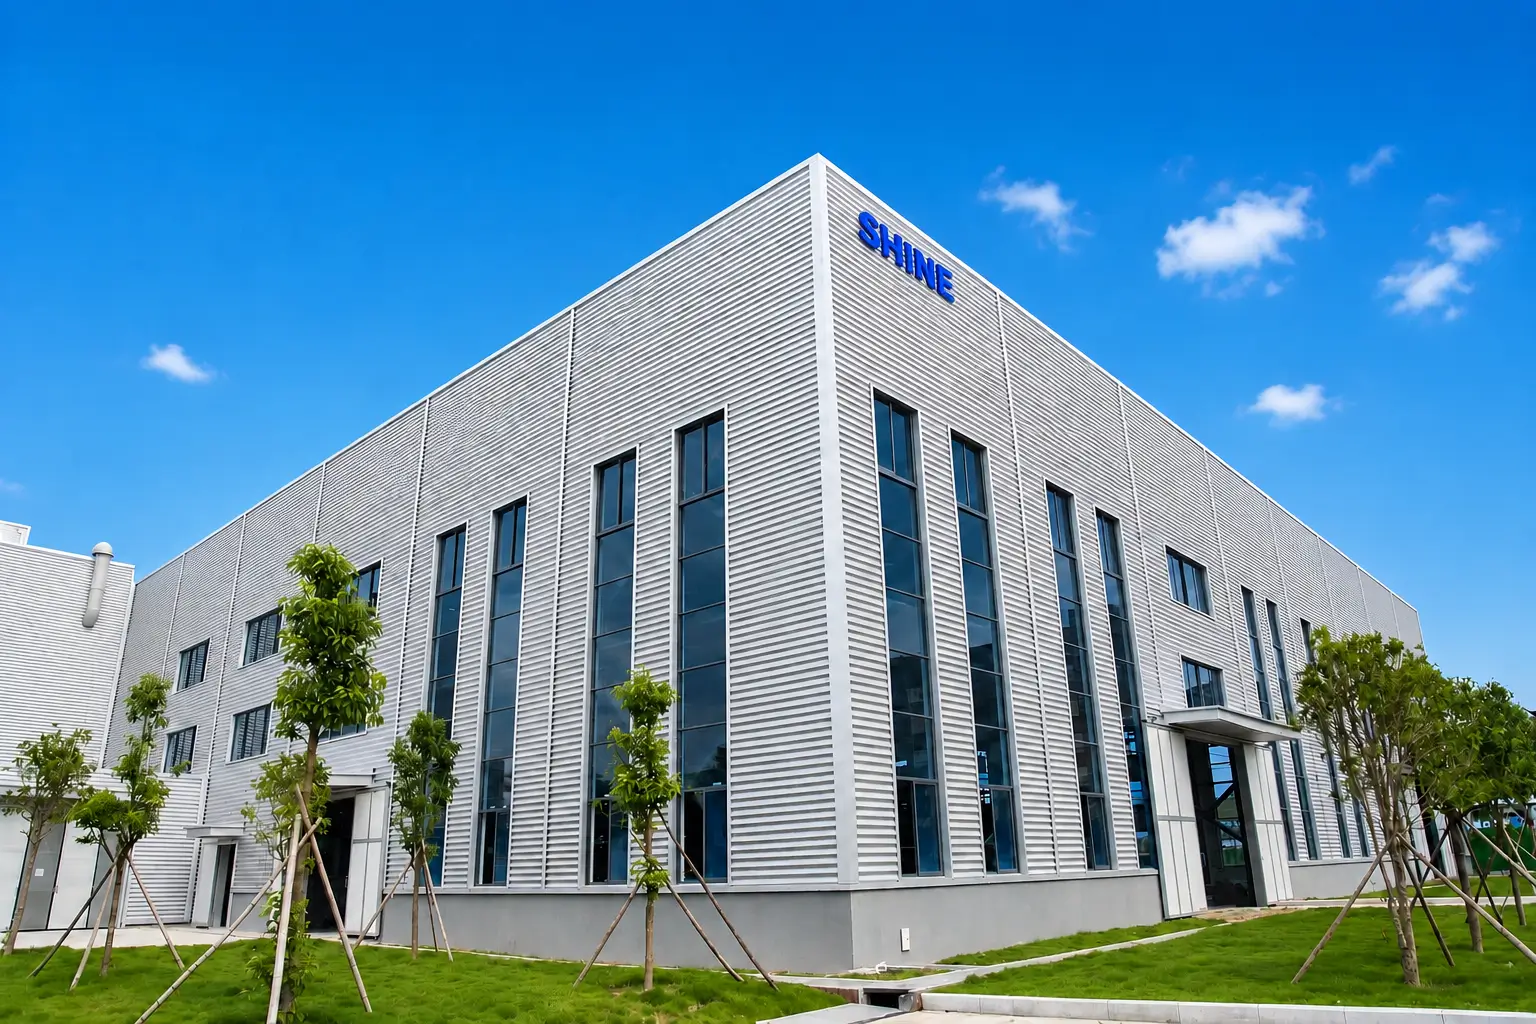
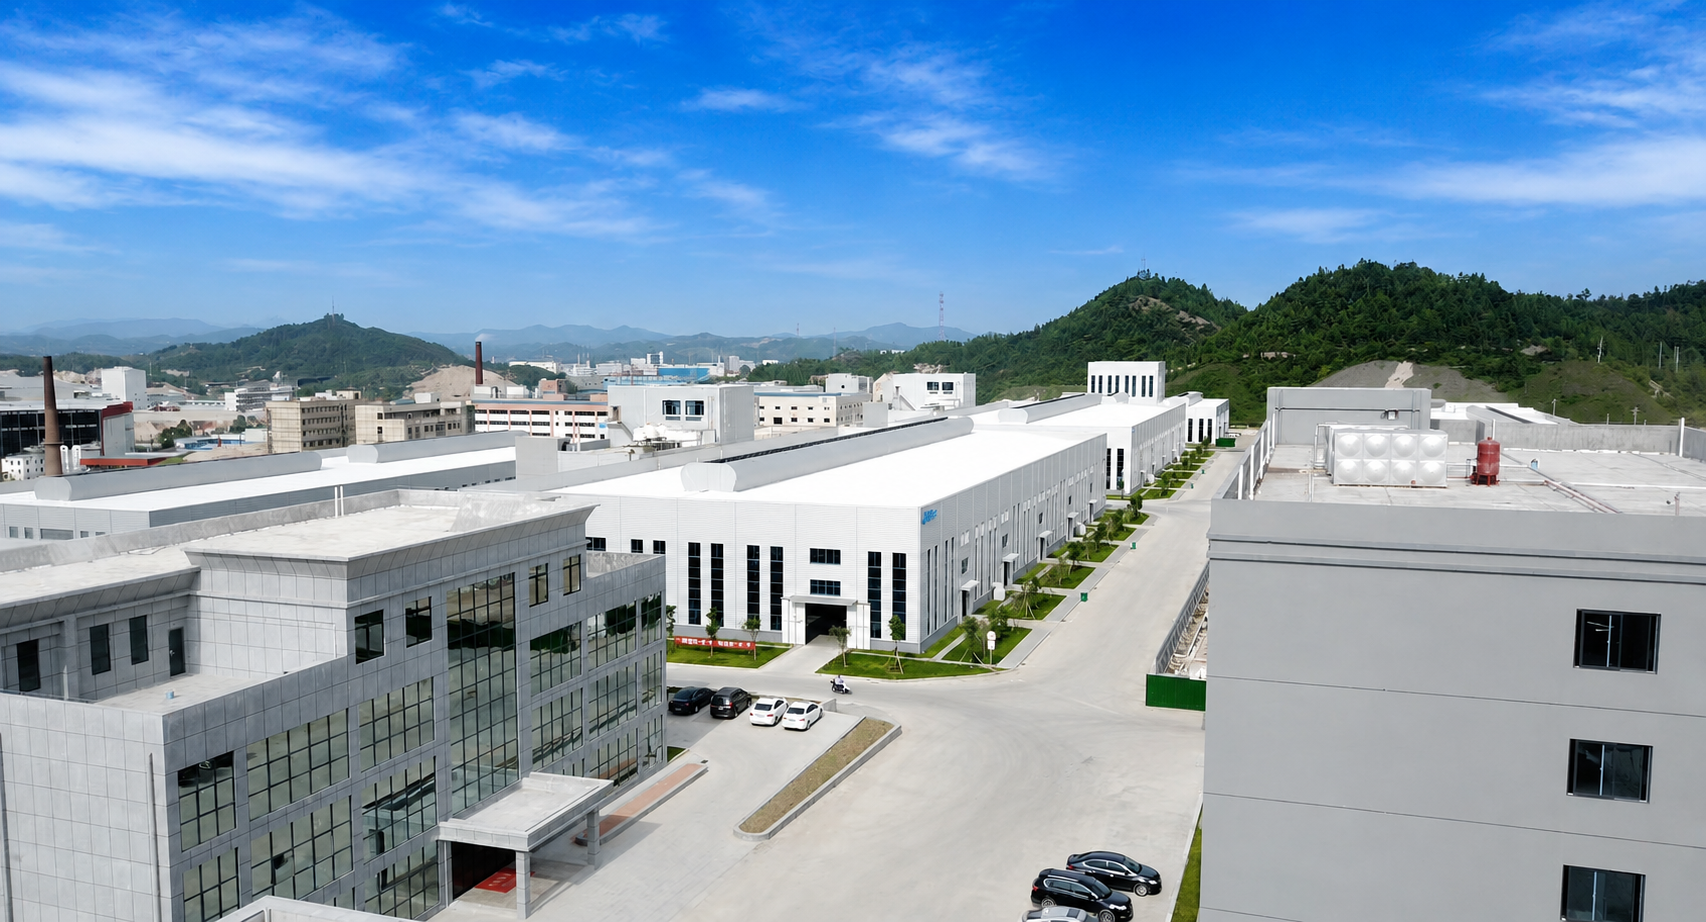
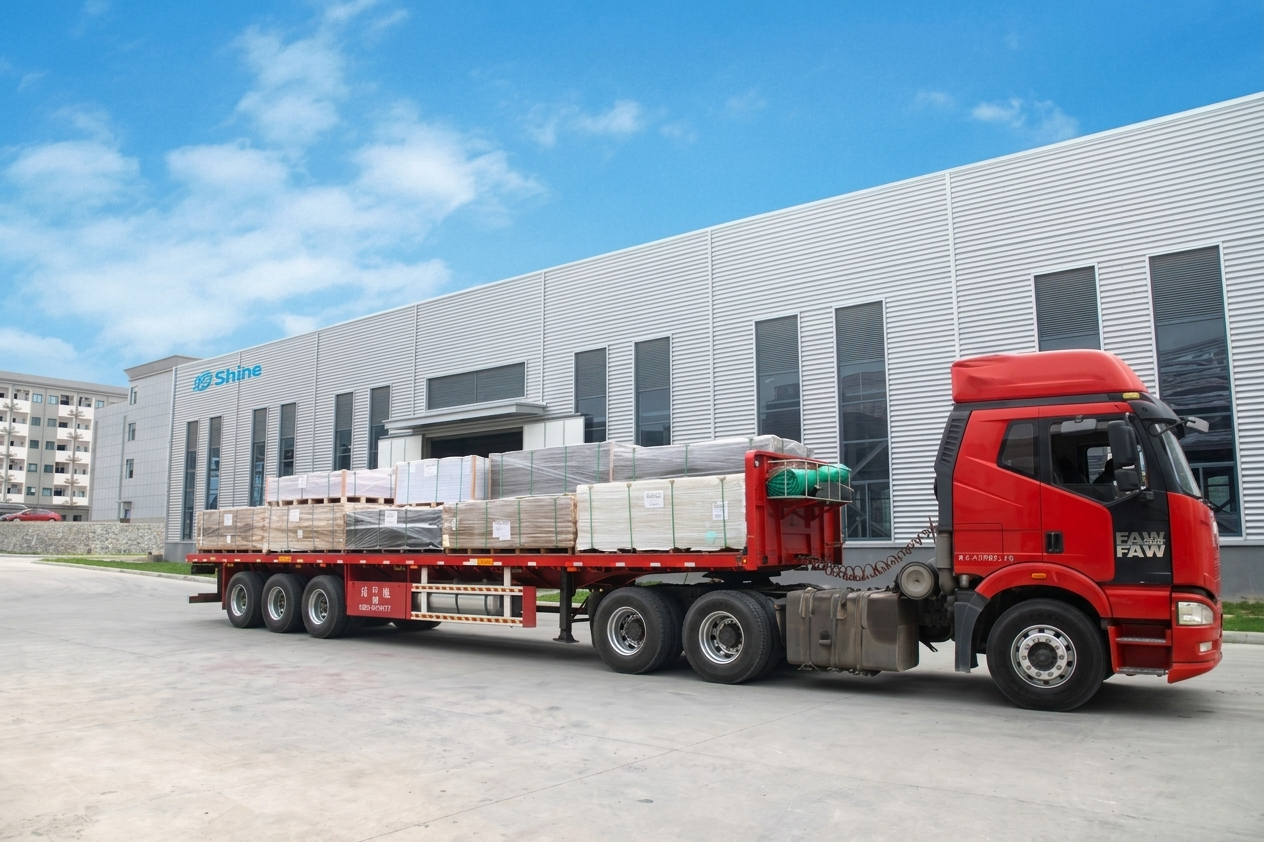
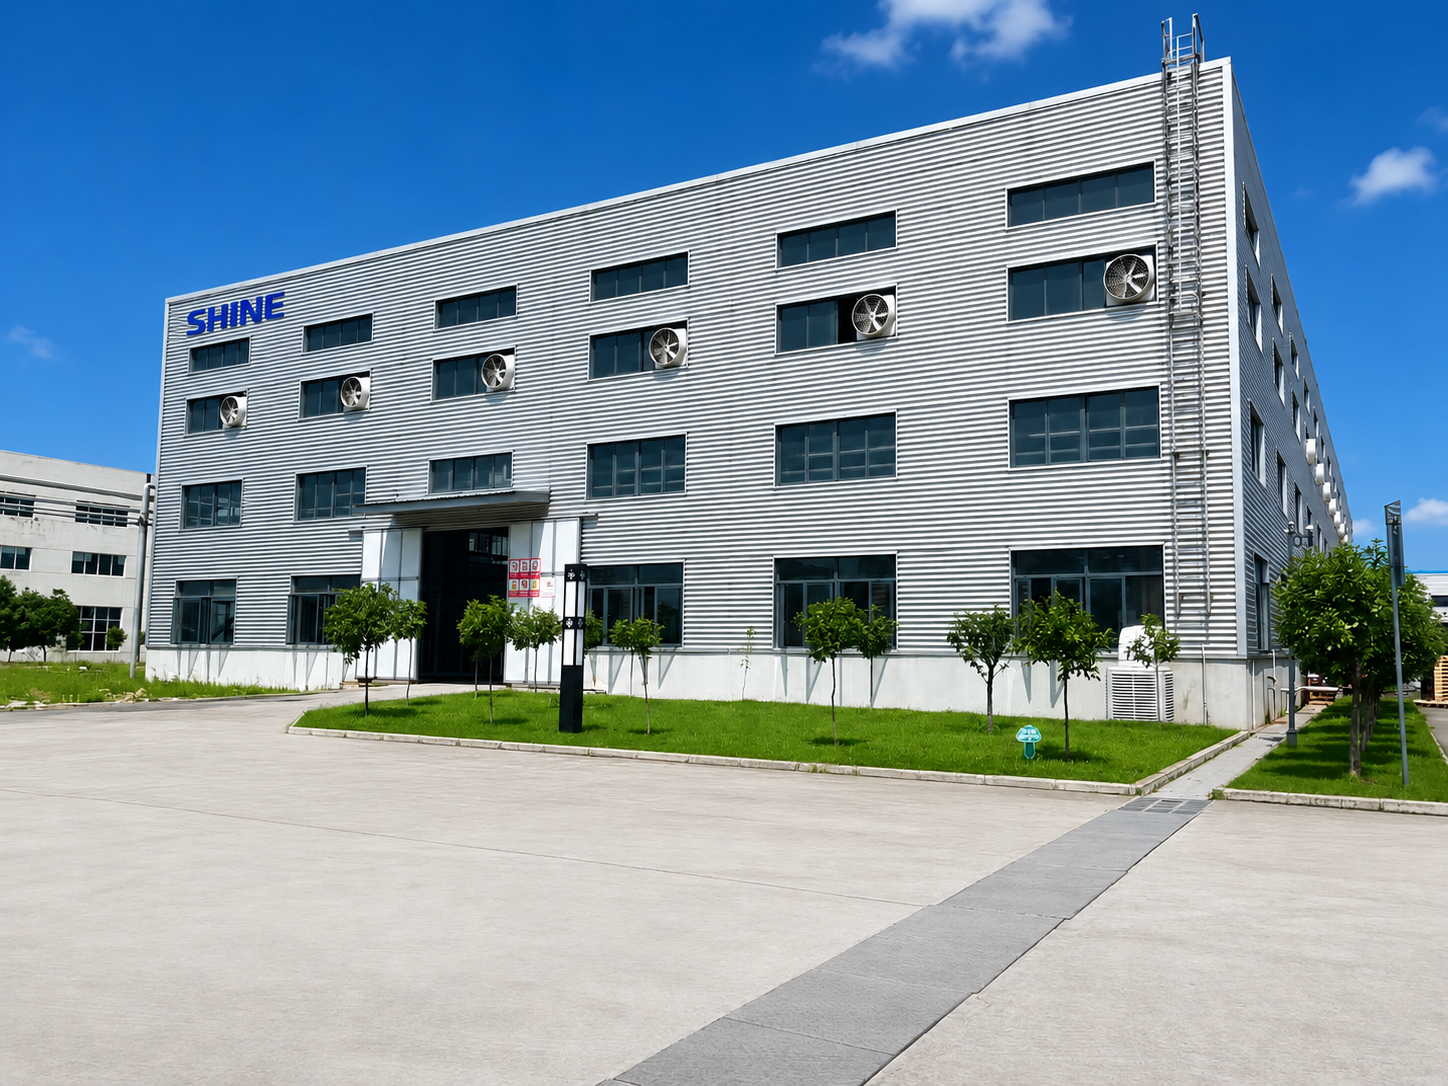
Shine Manufacturing Facility
Quality Standards & Compliance
Certified. Covers design, production, inspection, and delivery. This is not a certificate on the wall, it is the system that ensures the batch of Celuka you ordered in March machines the same way as the batch you ordered in September.
ISO 9001 Quality Management System
The raw materials used in Shine’s PVC formulations comply with both the RoHS requirement (lead ≤ 0.1% in homogeneous material) and the REACH declaration (lead content below 0.1% w/w).
Fire Rating DIN 4102 B1 and B2
For markets that require EN 13501-1 Euroclass classification, the products can meet Class C-s1,d0 or B-s1,d1 levels. Independent testing at a notified body is required according to product specifications. Shine can arrange this testing on behalf of the buyer, with testing costs borne by the buyer.
Third-Party Testing on Request
According to buyer requirements, testing by SGS, Bureau Veritas, RoHS, and TÜV can be arranged. The testing scope, standards, and timeline are confirmed prior to proceeding. Testing fees are borne by the buyer. This is standard industry practice. Do not trust a supplier who claims “all certifications included” unless they clearly specify the applicable standards, the testing body, and the year the report was issued.
Frequently Asked Questions
Answers to frequently asked questions about Shine products and services.
What does the hard skin actually do?
The hard skin is formed when the board surface is rapidly chilled during production. It is 0.1 to 1 millimetre thick with a hardness of Shore D65. It delivers three things: screw holding, clean CNC edges, and a surface that edge banding adhesives can grip. Without it, screws would not lock, cut lines would fuzz, and edge banding would not bond.
Can it support hinged doors and drawer slides?
It depends on density. At 0.55 g/cm³ and above, screw holding reaches 900N or higher, which is sufficient for standard cabinet hinges and drawer slides. Below 0.50, holding drops to between 500 and 700N, making it unsuitable for load-bearing components subject to repeated use. For bathroom vanity and kitchen cabinet boxes, specify 0.55 to 0.65 density. For door panels, 5 to 10 millimetre thickness.
Is it suitable for bathrooms and kitchens?
Yes. PVC does not absorb moisture. The closed-cell structure does not swell in humid conditions the way MDF does. This is the core advantage of Celuka board in bathroom vanities and kitchen cabinets. Pre-drill all screw holes. Leave a 5 millimetre ventilation gap at the cabinet base. For edge banding, use PUR hot melt adhesive with PVC edge banding tape. Lightly sand the skin with 400-grit paper before applying the adhesive.
Is B1 fire rating sufficient? What certification is needed?
B1 is the flame-retardant classification under DIN 4102-1, accepted for public buildings and commercial spaces in Germany and markets that follow European fire standards. If your project is in the Middle East, Southeast Asia, or other regions that do not reference DIN standards, confirm whether the local code accepts B1 or requires an EN 13501-1 Euroclass report. EN 13501-1 testing must be conducted by a notified body. Shine can arrange this at the buyer’s request. Testing fees are borne by the buyer. For the US market, independent UL 94 certification is required.
How long will it last outdoors?
Five to seven years. The hard skin provides a physical barrier against UV, but the skin itself contains no concentrated UV stabilisers. This is not a full-exposure outdoor material. Leave expansion gaps of 3 to 5 millimetres per metre. Use stainless steel fasteners with pre-drilled oversize holes. Dark-coloured boards can reach surface temperatures 15 to 25 degrees Celsius higher than white boards under direct sun and will age faster.
Can it be painted?
Yes. The hard skin is smooth, so sand it first with 400-grit paper. Clean with compressed air and isopropyl alcohol, then apply a plastic primer. Use only water-based acrylic or latex paint. Do not use oil-based or solvent-based paints. Apply thin coats in multiple passes. Full cure takes 30 days at 25 degrees Celsius. For outdoor painting, add a UV-resistant clear topcoat.
What are the minimum order quantity and lead times?
Standard specifications: 2 metric tons minimum, 7 to 14 days. Express orders: 3 to 5 days. Custom colour, density, thickness, or size: add 14 to 60 days. MOQ is by weight, not by sheet count. A thinner, lower-density sheet yields more panels per ton than a thicker one at the same dimensions.
The product comparisons, technical specifications, processing parameters, and application recommendations on this page are based on Shine’s current product range and internal testing data. Actual product performance varies by density, thickness, color, formulation, and operating conditions. The side-by-side comparison represents general product characteristics. Confirm specific performance values for your chosen specification before ordering. For project-specific evaluation, contact our team.
Related products
Take the Next Step
Three ways to move forward. Choose based on where you are in your sourcing process. We’ll respond within 1 business day.